We support Fast-Moving Consumer Goods (FMCG) manufacturers with real-time visibility, automated inventory management and compliance-focused digital solutions that connect production, materials, quality and warehouse operations.
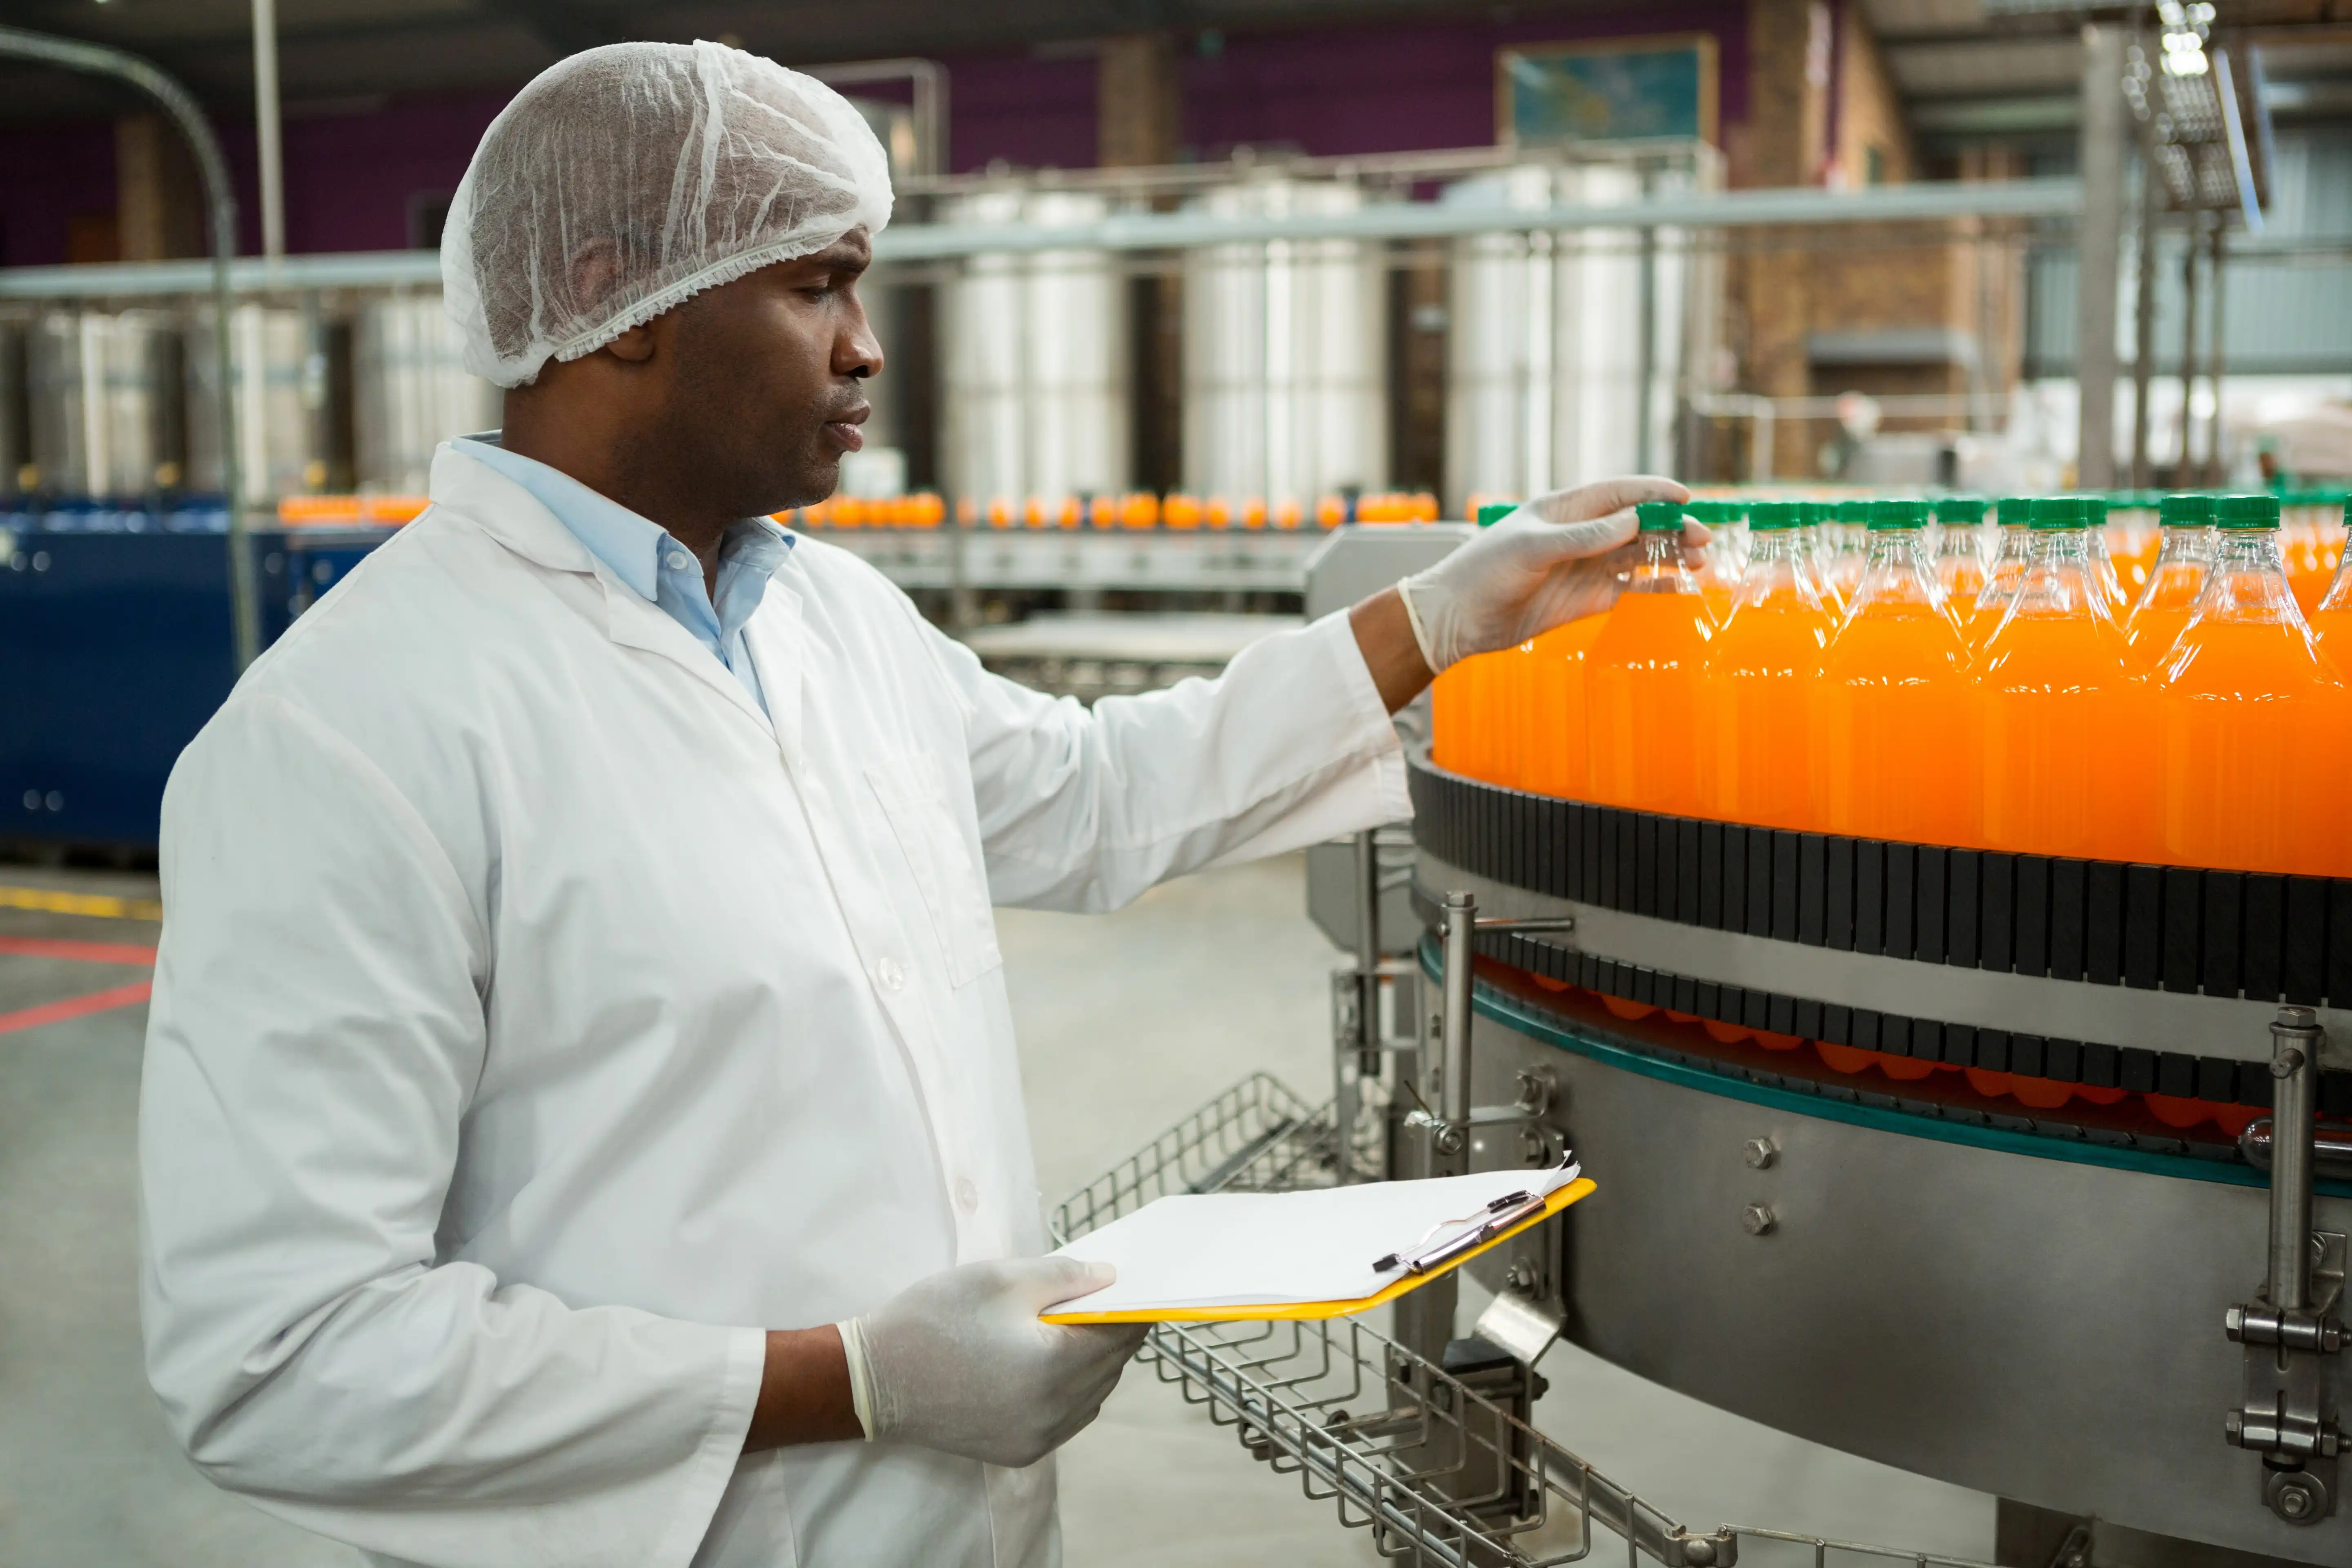
FMCG operations depend on consistent production output, fast-moving raw materials, packaging availability, accurate stock records and reliable product quality. When production, warehouse and quality data are maintained in separate systems, teams can face delayed updates, stock mismatches and limited visibility across manufacturing workflows.
SunBio IT Solutions develops industrial IoT, automation, AI/ML and custom software solutions that help manufacturers collect operational data, monitor connected equipment and organize information in centralized applications. The solution scope can be adapted to the plant's processes, existing machines and business systems.
Explore our Industry 4.0 solutions, Industrial IoT capabilities and custom industrial software.
Key Challenges in FMCG Manufacturing Operations
High-volume manufacturing and frequent product movement require coordination between production, stores, packaging, quality, dispatch and planning teams. Disconnected records can make it harder to respond quickly to changing operating conditions.
Limited Production Visibility
Manual updates and disconnected machine data can make it difficult to review line status, output and downtime as events occur.
Inventory Mismatches
Delayed stock updates can create uncertainty around raw materials, packaging materials, work-in-progress and finished goods.
Batch Traceability Gaps
Scattered production and material records can slow the process of tracing batches, lots and manufacturing events.
Quality Monitoring Delays
Quality readings and inspection outcomes may not be available to the right teams at the right time.
Compliance Documentation Effort
Manual logs and fragmented records can increase the effort involved in preparing operational and quality reports.
Unplanned Downtime
Without timely equipment and process information, maintenance teams may have less opportunity to identify developing issues.
Our FMCG Manufacturing & Digital Operations Solutions
SunBio combines connected sensors, machine interfaces, industrial gateways, automation and custom applications to build practical visibility across FMCG production and supply operations.
Real-Time Production Monitoring
Collect selected machine and line information to monitor production status, output, cycle events and downtime through a centralized dashboard.
Automated Inventory Management
Connect inventory transactions and sensor-based readings where suitable to improve visibility of raw materials, packaging, work-in-progress and finished goods.
Batch & Lot Traceability
Organize batch identifiers, material consumption, production timestamps and selected process events to support traceability across manufacturing stages.
Quality & Process Monitoring
Integrate suitable sensors, inspection inputs and process readings to help teams review quality parameters and configured threshold exceptions.
Packaging Line & Visual Inspection
Use automation and AI vision workflows, where appropriate, to support checks such as label presence, packaging defects, product counts and selected visual quality conditions.
Explore our image analytics and AI vision solutions.
Warehouse & Cold-Storage Monitoring
Monitor selected storage conditions such as temperature and humidity, and bring warehouse events into a shared operational view when product requirements call for it.
Compliance Records & Digital Reporting
Capture time-stamped production, inspection and process records to support consistent documentation, searchable history and report preparation. Regulatory requirements should be mapped to the manufacturer's applicable standards and procedures.
Centralized Dashboards & System Integration
Bring machine, sensor and application data together using suitable APIs, industrial protocols and messaging connectivity, with integration scope based on the existing environment.
Production, Inventory & Compliance Visibility
A connected FMCG operations platform can combine information from multiple stages of the manufacturing workflow. The exact data points and automation rules depend on the product, production process, available machine interfaces and the manufacturer's quality procedures.
Capture Production & Sensor Data
Collect selected machine states, counters, process readings and environmental measurements from connected equipment and sensors.
Connect Material & Batch Events
Associate relevant material movements, lot numbers and production events with the applicable process or batch records.
Process Rules & Exceptions
Apply configured business rules for stock thresholds, production exceptions, quality readings and workflow notifications.
Review Dashboards & Reports
Provide authorized teams with a consolidated view of production, inventory, quality events and relevant digital records.
Learn how industrial automation and AI/ML services can complement connected manufacturing workflows.
Benefits of Connected FMCG Manufacturing
When designed around real plant workflows, connected systems can help teams access timely information, reduce manual coordination and make operational records easier to review.
Better Production Visibility
Review line status, output and selected process events from a centralized interface.
Improved Stock Awareness
Make raw material, packaging and finished-goods information easier to access and reconcile.
Stronger Batch Traceability
Organize batch and lot-related information across relevant production steps.
Timely Exception Alerts
Notify responsible teams when configured thresholds or workflow conditions require attention.
Consistent Digital Records
Reduce dependence on scattered manual logs by maintaining structured operational data.
Data-Led Decisions
Use consolidated production and inventory information to support planning and continuous improvement.
FMCG Industry Applications
Connected monitoring and automation can be adapted to different fast-moving consumer goods categories and production environments.
Food & Beverage
Production-line monitoring, batch records, storage-condition monitoring and packaging inspection.
Personal Care & Cosmetics
Material tracking, filling and packaging line visibility, quality checkpoints and batch traceability.
Home & Fabric Care
Process monitoring, inventory visibility, packaging verification and production reporting.
Consumer Packaged Goods
Finished-goods tracking, warehouse movement visibility, dispatch records and stock monitoring.
Pharma-Adjacent Consumer Products
Configured process and documentation workflows for applicable non-prescription consumer product operations, aligned with the manufacturer's requirements.
Multi-Site Manufacturing
Consolidated dashboards that help authorized teams review selected metrics across plants and locations.
Our FMCG Solution Implementation Approach
We begin with the operational requirement and existing plant environment, then define a practical integration and deployment plan.
Understand the Production Workflow
Review production stages, inventory hand-offs, quality checkpoints, reporting needs and operational pain points.
Identify Data & Device Requirements
Map available machine interfaces, sensors, gateways, identifiers and connectivity requirements.
Design Integration & Application Logic
Define data flows, dashboards, alerts, batch records and integration points with compatible business systems.
Validate in the Operating Environment
Test data accuracy, device communication, user workflows and exception handling against agreed requirements.
Deploy & Improve
Roll out the agreed solution, review operational feedback and refine dashboards, alerts and integrations as needs evolve.
Why Choose SunBio IT Solutions for FMCG Manufacturing?
SunBio IT Solutions works across industrial IoT, automation, AI/ML and custom software development. We focus on connecting relevant operational data with applications that fit the manufacturer's actual workflow.
Industrial IoT & Connectivity
Connect suitable sensors, devices, gateways and machine data sources.
Custom Software Development
Build dashboards, data workflows, reports and integrations around project requirements.
AI & Image Analytics
Explore vision-based inspection and counting use cases where visual automation is appropriate.
Integrated Approach
Bring hardware connectivity, data processing and application development into one project scope.
Visit our About SunBio page to learn more about our industrial technology focus.
Build a More Connected FMCG Manufacturing Operation
Looking to improve production visibility, automate inventory updates, strengthen batch traceability or connect quality data? Discuss your FMCG manufacturing requirements with SunBio IT Solutions.